Computer Vision Technologies Used in Industrial Video Analytics
A single camera overlooking a production floor captures thousands of visual details every minute. Workers move between stations, forklifts transport materials, machines operate at different speeds, and finished products travel through multiple inspection points. While every activity is visible, extracting meaningful information from this continuous stream is impossible through manual observation alone.
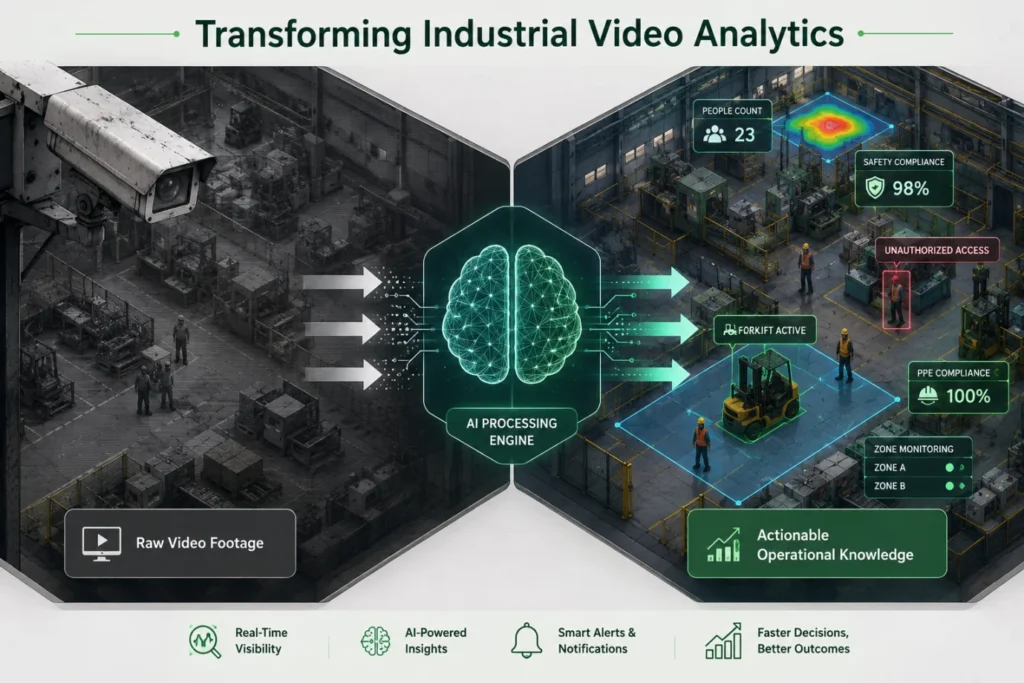
Computer Vision provides the analytical capability that transforms industrial video into operational knowledge. Instead of treating CCTV footage as archived recordings, Industrial AI interprets images, recognizes activities, identifies exceptions, and supplies information that supports production, quality, safety, and facility management. Understanding the technologies behind this process helps decision-makers evaluate how Industrial Video Analytics contributes to everyday operations.
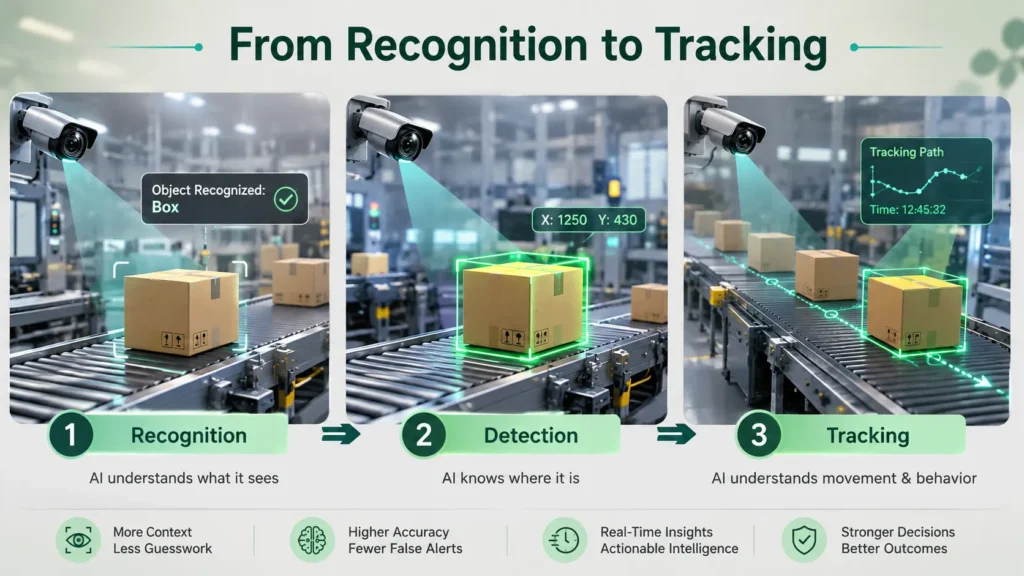
Image Recognition: Identifying Industrial Assets
Recognizing objects in a camera’s area of view is the initial step in computer vision.
Depending on the operational environment, AI can identify:
- Personnel
- Machinery
- Vehicles
- Tools
- Raw materials
- Finished products
- Safety equipment
- Industrial containers
Accurate object recognition provides the foundation for every higher-level analysis performed by the system.
Object Detection: Locating Critical Elements
Recognizing an object is only part of the task. AI also determines where each object is located within the scene and tracks its position over time.
Typical industrial applications include:
- Detecting forklifts near pedestrian pathways
- Identifying pallets within storage areas
- Locating safety cones and barriers
- Monitoring equipment occupancy
- Tracking material movement between workstations
- Identifying missing safety equipment
Location awareness allows operational events to be evaluated within their physical context.
Object Tracking: Following Activities Over Time
Industrial operations involve movement rather than isolated images. Object tracking enables AI to follow people, vehicles, or equipment across multiple video frames.
Examples include:
- Monitoring forklift travel routes
- Following operator movement inside production zones
- Tracking material transfer between stations
- Observing inspection workflows
- Recording vehicle entry and exit
- Monitoring equipment utilization
Tracking provides a continuous understanding of operational activities instead of disconnected snapshots.
Scene Understanding: Interpreting Workplace Conditions
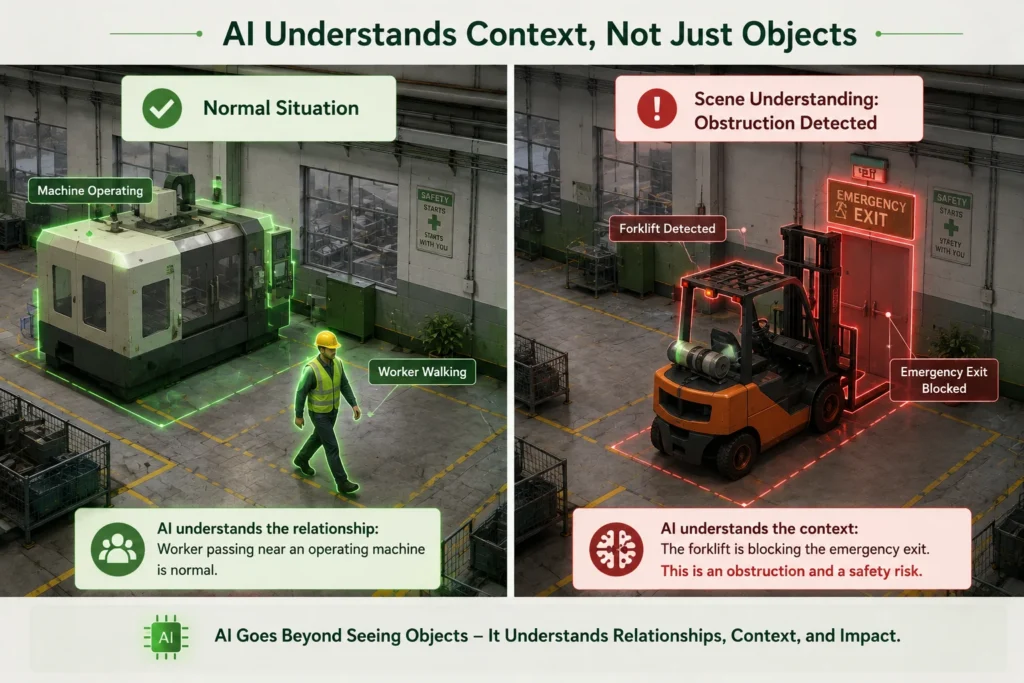
Computer Vision evaluates relationships between multiple objects rather than analysing each object independently.
Workplace Situation | Computer Vision Interpretation |
Worker near operating machine | Equipment interaction identified |
Vehicle enters restricted area | Location rule evaluated |
Material blocks emergency exit | Obstruction detected |
Multiple people gather unexpectedly | Occupancy condition assessed |
Safety barrier removed | Workplace condition changed |
Product remains stationary | Process interruption suspected |
This broader interpretation helps distinguish routine operations from situations requiring attention.
Action Recognition: Understanding Operational Tasks
Many industrial decisions depend on recognising what people are doing rather than simply identifying who is present.
Computer Vision can evaluate activities such as:
- Manual assembly
- Material loading
- Equipment operation
- Product inspection
- Machine servicing
- Safety procedure execution
- Packaging operations
- Cleaning activities
Action recognition supports SOP verification by comparing observed behaviour with expected work practices.
Anomaly Detection: Identifying Unusual Events
Industrial facilities cannot anticipate every possible operational situation through predefined rules. Anomaly detection focuses on identifying behaviour that differs significantly from established operating patterns.
Examples include:
- Unexpected movement within restricted zones
- Equipment operating outside normal schedules
- Objects appearing in unusual locations
- Irregular pedestrian traffic
- Abnormal production flow
- Unusual equipment interaction
This capability assists supervisors in discovering events that may otherwise remain unnoticed.
Visual Measurement and Counting
Computer Vision can also perform repetitive measurement tasks that traditionally require manual observation.
Common applications include:
- Counting products
- Measuring queue lengths
- Monitoring occupancy levels
- Tracking production quantities
- Verifying pallet counts
- Estimating vehicle movement
- Monitoring workstation utilization
- Recording loading activities
Automating these observations improves reporting consistency while reducing manual data collection.
Combining Visual Intelligence with Operational Data
The greatest operational value emerges when Computer Vision works alongside other industrial systems instead of functioning independently.
Information may be combined with:
- PLC operating signals
- SCADA data
- IoT sensor measurements
- Equipment status
- Production schedules
- Energy monitoring systems
- Maintenance records
- AI Dashboards
Combining these data sources gives managers a more comprehensive picture of the facility’s operational state.
Operational Perspective
Management Need | Computer Vision Contribution |
Process verification | Observes whether operational procedures are followed |
Workplace Safety | Detects unsafe conditions and behavioural deviations |
Production oversight | Monitors movement of materials and equipment |
Quality management | Supports visual inspection and process consistency |
Facility supervision | Provides continuous observation across operational areas |
Performance reviews | Generates measurable visual observations for analysis |
Looking Beyond Individual Cameras
The value of Computer Vision is not determined by the number of cameras installed but by the quality of the operational understanding those cameras provide. When visual observations become structured information, managers gain clearer insight into workplace activities, process execution, and resource utilization. Integrated with AI Video Analytics, Edge AI, Intelligent CCTV Monitoring, Industrial AI, Operational Intelligence, and Real-Time Analytics, Computer Vision becomes an important source of evidence for informed industrial decision-making rather than simply a tool for recording events.
FAQs
Does Computer Vision require specialised industrial cameras?
No. Many Computer Vision applications can operate using existing IP CCTV cameras, provided the video quality is suitable for the intended analysis.
What distinguishes object detection from object tracking?
Object detection identifies an object within a video frame, while object tracking follows that object’s movement across consecutive frames.
Can Computer Vision recognise both people and industrial equipment simultaneously?
Yes. Modern Computer Vision models can identify and analyse multiple object categories within the same scene.
Is anomaly detection based only on predefined rules?
No. Depending on the implementation, anomaly detection can identify unusual patterns that differ from normal operational behaviour, even if a specific rule has not been configured.
Which industrial processes commonly use visual measurement?
Visual measurement is widely used for production counting, occupancy monitoring, material tracking, packaging verification, loading operations, and workflow analysis.